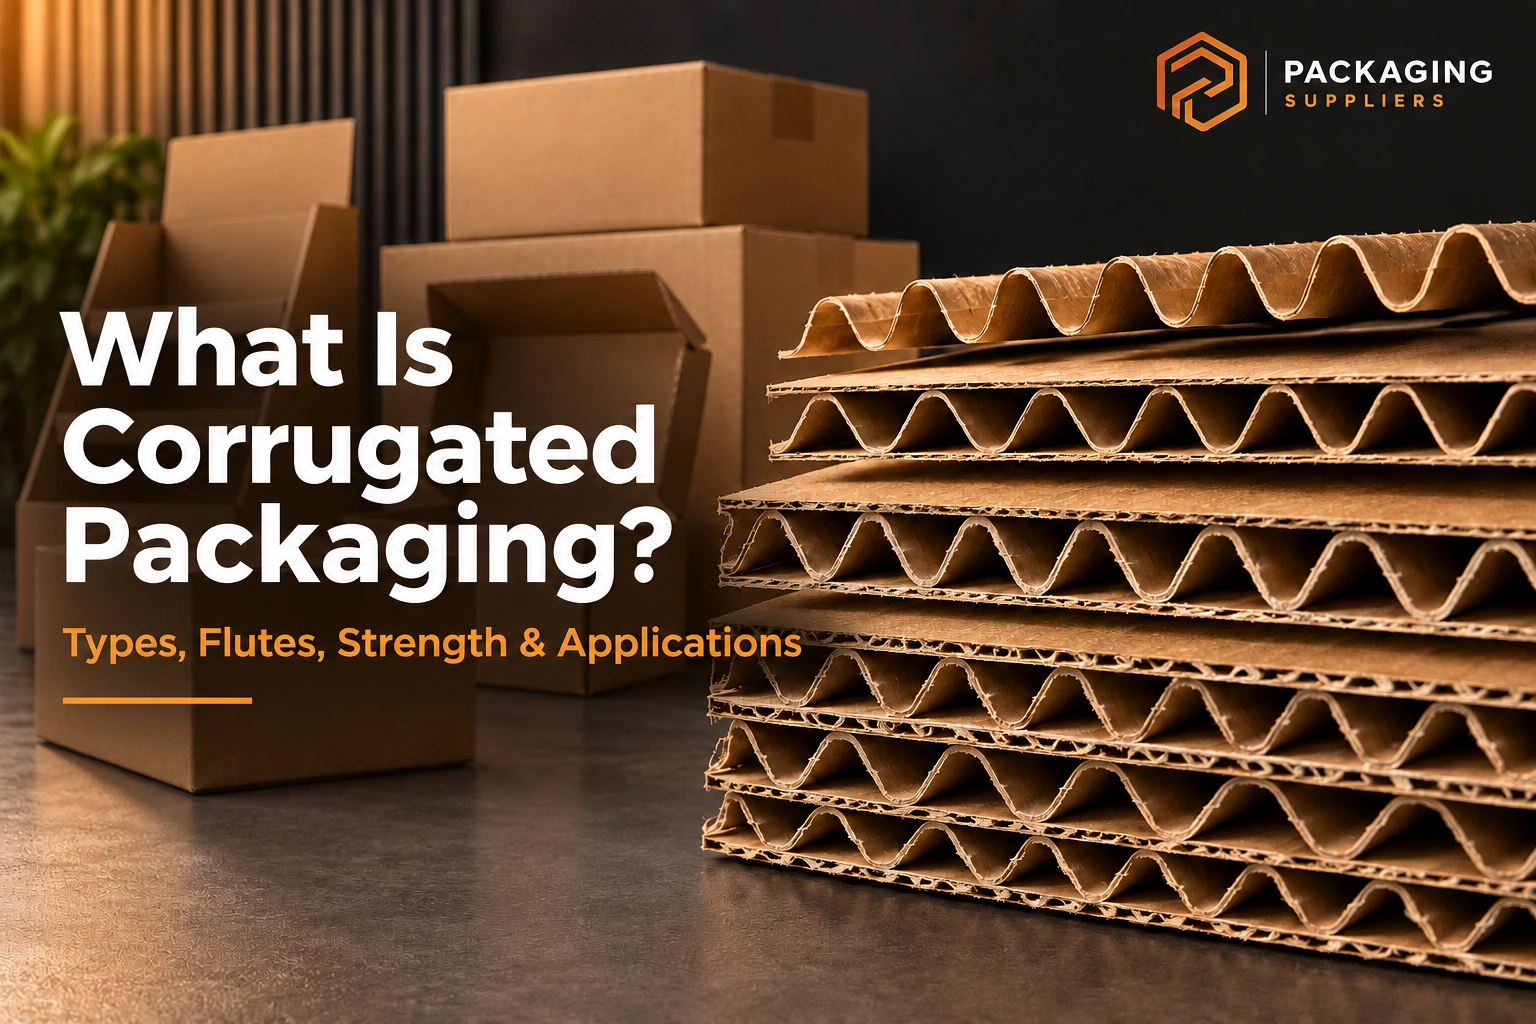
Corrugated packaging is made from corrugated fiberboard, a structure in which one or more wave-shaped paper media are bonded to flat linerboards. The flutes act like repeated arches, creating thickness, bending stiffness, cushioning and edgewise compression resistance with less fiber than a solid sheet of similar caliper. This is why corrugated board is widely used for shipping boxes, mailers, trays, displays, partitions and bulk containers.
For the wider context of packaging levels, functions and formats, see what packaging is.
Corrugated board is used for shipping cases, e-commerce mailers, retail-ready trays, displays, partitions, inserts, bulk bins and heavy-duty industrial packs. Its performance depends on the papers, flute profile, number of walls, adhesive, board grade, box style, dimensions, manufacturing quality and the environment in which it is used.
Corrugated packaging in one minute
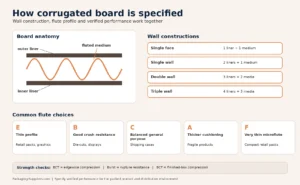
- Construction tells you how many liners and fluted media are present: single face, single wall, double wall or triple wall.
- Flute letter describes approximate flute geometry; it does not by itself state box strength.
- ECT measures an edgewise board property, burst measures rupture resistance, and BCT measures a finished box under compression.
- The correct specification combines board performance, box style, dimensions, product support, climate and distribution testing.
Corrugated packaging at a glance
| Term | Meaning |
| Linerboard | The flat paper facings on the outside or between fluted media |
| Corrugating medium | Paper formed into repeating arches or flutes |
| Single face | One liner bonded to one fluted medium |
| Single wall | One fluted medium between two liners |
| Double wall | Two fluted media separated by three liners |
| Triple wall | Three fluted media separated by four liners |
| Flute profile | The approximate height and spacing of the arches |
| ECT | Edge Crush Test, measuring edgewise compression resistance of a board specimen |
| Burst strength | Resistance of board to rupture under hydraulic pressure |
| BCT | Box Compression Test, measuring the compression capacity of a finished box |
How corrugated board is made
A corrugator heats and conditions the medium, forms it around fluted rolls and applies starch-based adhesive to the flute tips. The medium is first bonded to a liner to make single-face web, then bonded to another liner to create single-wall board. Additional media and liners create double- or triple-wall board. The combined board is dried, slit and cut into sheets before printing, scoring, die-cutting, folding and joint formation.
Corrugated cardboard and paperboard are not the same
Everyday speech often calls any brown box cardboard, but the structures differ. Paperboard is generally a solid fiber sheet used for folding cartons and sleeves. Corrugated fiberboard contains a visibly fluted medium between linerboards. That structure gives corrugated board greater thickness and stiffness for shipping and load-bearing applications.
To compare corrugated with plastic, glass, metal, wood and other options, see our packaging materials guide.
Advantages and limitations of corrugated packaging
Advantages
- High stiffness-to-weight ratio for shipping, stacking and product protection.
- Fluted structure provides cushioning and can be engineered with different wall and flute combinations.
- Easy to print, die-cut and convert into shipping cases, mailers, trays, displays and inserts.
- Ships and stores efficiently as flat blanks for many box styles, and fiber-based formats are widely collected in many markets.
Limitations
- Humidity, liquid water and condensation can reduce compression strength unless the structure is designed for those conditions.
- Edges, scores, hand holes, display cut-outs and poor palletization can create weak points even when the board grade is adequate.
- Thicker corrugated structures can use more storage cube than thin flexible packaging, and some products require liners, coatings or inner packs for barrier or direct-contact needs.
- A flute letter or wall count alone is not a finished-box performance specification.
Types of corrugated board by wall construction
1. Single face
Single-face board has one liner and one exposed fluted medium. It is flexible and commonly used as a wrap, pad, separator or cushioning layer rather than as a self-supporting shipping case.
2. Single wall
Single-wall board places one fluted medium between two liners. It is the most familiar construction for regular slotted containers, die-cut mailers, trays and displays. Strength can vary substantially across flute profiles and board grades.
3. Double wall
Double-wall board uses two fluted media and three liners. Combining two flute profiles can improve puncture resistance, stiffness, cushioning and stacking performance. It is used for heavier goods, demanding distribution and retail displays that need more rigidity.
4. Triple wall
Triple-wall board uses three fluted media and four liners. It can replace wood in some bulk and industrial applications, but the complete pack still needs engineering for the load, handling method, pallet, climate and journey.
How many Corrugated flute are there
A flute letter describes approximate flute geometry, not a strength grade. C flute is a common general-purpose shipping profile, B flute is often used where die-cutting and panel crush behavior matter, and E flute is a thinner microflute used for compact printed structures. Exact caliper and flute count vary by corrugator and board combination. For a side-by-side selection guide, see E-Flute vs B-Flute vs C-Flute Corrugated Packaging.
What determines corrugated strength
Paper properties and basis weights
Liner and medium furnish, basis weight, recycled-fiber content, moisture and manufacturing consistency influence board performance. Recycled content by itself does not tell a buyer how a finished box will perform; the relevant test results and production controls matter.
Flute profile
Flute profile affects thickness, print surface, cushioning and crush behavior, but it does not define box strength by itself. Use the dedicated E-, B- and C-flute comparison for detailed profile selection.
Wall construction
Adding walls can increase stiffness, puncture resistance and compression performance, but also increases caliper, material and storage volume. A well-designed single-wall case may outperform a poorly designed double-wall case for a particular load.
Box dimensions and style
Panel proportions, depth, flap design, score placement, die-cut openings and manufacturer’s joint all affect performance. Tall narrow boxes can buckle differently from compact cases. Hand holes and large display cut-outs remove load-bearing material and may require reinforcement or a stronger board.
Moisture time and stacking pattern
Paper fibers respond to relative humidity, and sustained loads cause creep. Warehouse duration, refrigerated conditions, condensation and pallet overhang can reduce stacking capacity. Column-aligned stacks usually carry compression more effectively than interlocked patterns, although unit-load stability must also be considered.
How corrugated strength is specified
In U.S. corrugated specifications, ECT reports edgewise compression resistance of the board in lb/in, burst reports rupture resistance, and BCT measures a finished box under compression. They are different measures, and none should be inferred from flute letter alone. Finished performance also depends on box dimensions, style, humidity, workmanship and the contents. For the detailed relationship between flute choice and these tests, see E-Flute vs B-Flute vs C-Flute.
Common corrugated box styles
- Regular slotted container for efficient general shipping
- Full-overlap and half-slotted cases for specific protection or loading needs
- Die-cut mailers for e-commerce and subscription products
- Five-panel folders and wraps for long or shallow items
- Trays and display-ready cases for retail replenishment
- Bulk bins and pallet boxes for produce, parts and industrial goods
- Partitions, pads and fitted inserts for separation and cushioning
Common U.S. box styles: start with the RSC
The regular slotted container (RSC) is one of the most common U.S. corrugated shipping-case styles. FBA/PMMI define it as a single-sheet container with four panels and top/bottom flaps, with the outer flaps meeting at the center when closed. U.S. buyers commonly specify the style by name or acronym; an international FEFCO code such as 0201 can be added when drawings or cross-border suppliers use that system, but it should not replace the dimensions and performance specification. FBA/PMMI RSC reference
Applications by industry
Food and beverage businesses use corrugated cases, produce trays, dividers and displays. E-commerce brands use mailers and shipping cases sized for parcel networks. Electronics and appliances use corrugated with engineered cushioning or partitions. Automotive and industrial suppliers use heavy-duty cases, bulk bins and corrosion-control systems. Retailers use printed displays and shelf-ready trays that protect products until the case is opened in store.
Printing and finishing options
Corrugated packaging can be flexographically printed, litho-laminated or digitally printed. Kraft and white liners create different visual results. Coatings may improve scuff, moisture or grease resistance. Print method should be matched to order volume, color expectations, variable artwork, lead time and the surface quality of the chosen flute.
How to specify corrugated packaging
- Record product dimensions, mass, center of gravity, fragility and sensitivity.
- Define the packing pattern, internal support and required headspace.
- Map parcel, freight, pallet, warehouse and climate hazards.
- Choose a box style that supports loading, closing, opening and return needs.
- Set board performance using appropriate ECT, burst, caliper or supplier grade requirements.
- Identify flute or wall construction only after performance and converting needs are clear.
- Prototype and test filled production-representative packs.
- Confirm print, coatings, adhesives, tolerances, pallet pattern and quality checks.
- Approve a specification that controls both material and finished-box requirements.
Worked specification example
Suppose a business needs to ship twelve filled glass jars by pallet and occasional parcel. A useful brief would state jar dimensions and mass, divider arrangement, box internal dimensions, pallet pattern, maximum stack height, warehouse duration, humidity range and parcel frequency. The supplier could then compare single-wall and double-wall options, select an ECT or alternative board grade, prototype the partition and validate compression and drops. Asking only for a “C-flute box” would leave nearly every performance variable undefined.
Common specification mistakes
- Choosing flute letter before defining the load and distribution hazards.
- Copying an ECT or burst value from an old box without confirming dimensions or contents.
- Using outside dimensions when the product and inserts require controlled internal space.
- Ignoring humidity, cold-chain condensation, storage time or pallet overhang.
- Approving a hand sample but not production tolerances, score position and joint quality.
- Testing an empty box when the contents add support, concentrate loads or change drop behavior.
Testing corrugated shipping systems
A packaging test plan may include conditioning, compression, drop, impact and vibration. ASTM D4169 and ISTA procedures are commonly referenced frameworks for distribution testing, while ASTM D642 covers compression testing and ASTM D4332 covers conditioning atmospheres. The correct schedule and assurance level depend on the distribution system, product risk and validation objective. ASTM D4169-23e1 | ISTA procedures | ASTM D642-25 | ASTM D4332-22
Test the system that will actually ship
Condition samples to the relevant environment, use production board and closures, and pack them with representative products or validated dummies. Parcel and palletized freight do not create the same hazards, so the test sequence should match the route. Record failure modes rather than only pass or fail: crushed corners, score-line buckling, divider collapse, product contact and closure opening each point to a different design change.
Corrugated packaging and sustainability
Corrugated board is fiber-based and widely collected in many markets, but performance and recovery depend on the complete pack. Minimize avoidable material, keep coatings and attachments compatible with the intended recovery route, right-size the case and prevent product damage. Reuse can be appropriate when the case remains structurally sound and the return system supports enough cycles.
Claims should avoid universal recycling percentages or acceptance statements unless they are current, sourced and relevant to the sales geography. Collection rules differ, and wet, waxed or heavily contaminated cases may not be accepted with clean old corrugated containers.
Manufacture corrugated packaging to a defined specification
Need corrugated packaging built around your product and shipping requirements? Packaging Suppliers provides manufacturer-led corrugated solutions, with in-house production for suitable constructions and trusted production partners for specialized formats or processes. Share your product weight, inside dimensions, shipment route, print requirements, and performance needs, and we’ll recommend the right board, flute, box style, and production route. Request a quote or sample to confirm fit, strength, and print quality before production.
Conclusion
Corrugated packaging gains its efficiency from a fluted medium bonded to linerboards. Wall construction and flute profile shape the board, while paper properties, box design, humidity and manufacturing quality determine real performance. A reliable specification connects ECT, burst or box-compression requirements to the packed product and verifies the complete design under representative distribution conditions.
Frequently asked questions
What is corrugated packaging made from?
It is made from flat linerboards bonded to one or more wave-shaped corrugating media. The papers and adhesive form corrugated fiberboard.
What is the difference between cardboard and corrugated?
Cardboard is an informal term that may include solid paperboard. Corrugated board has a fluted medium between liners, giving it more thickness and structural stiffness.
Which corrugated flute is strongest?
No flute is universally strongest. Strength depends on the full board grade, papers, wall construction, box style and conditions. A and C flutes are thicker; B and E can offer crush resistance and better print or die-cut characteristics.
What does 32 ECT mean?
In common U.S. corrugated specifications, 32 ECT means the board is rated at 32 lb/in of edge-crush resistance under the applicable test method. It is a board property, not a statement that the finished box can safely stack or carry 32 pounds; box geometry, contents, humidity, workmanship and distribution conditions still matter. Fibre Box Association ECT guidance
Is double-wall corrugated always better than single-wall?
No. Double wall can add stiffness and protection, but it also adds material and caliper. A properly specified single-wall board may be sufficient and more efficient for a lighter product or shorter distribution journey.
Can corrugated packaging get wet?
Standard corrugated board loses performance as it absorbs moisture. Water-resistant papers, coatings and adhesives can improve performance, but exposure conditions and recovery implications should be reviewed.
How should a corrugated box be measured?
Boxes are generally specified by internal length, width and depth in that order. Confirm the supplier’s measurement convention and allow space for the product, inserts and packing tolerance.
Sources and standards
References used in the article:
- FBA/PMMI — Regular Slotted Containers (RSC) technical reference
- ASTM D4169-23e1 — Performance Testing of Shipping Containers and Systems
- ISTA — Test Procedures
- ASTM D642-25 — Compressive Resistance of Shipping Containers
- ASTM D4332-22 — Conditioning Packages for Testing
- Fibre Box Association — Edge Crush Test Guide